

2026-10-22
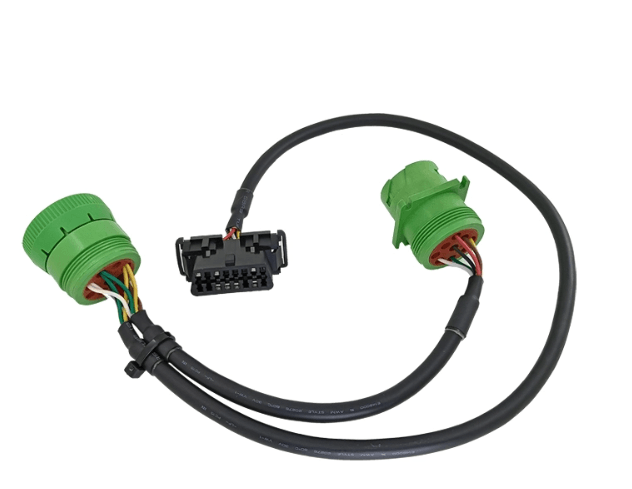
The modern vehicle is no longer just a mechanical machine; it is a sophisticated electronic ecosystem. At the heart of this system lies the automotive wire harness—a complex network of cables, terminals, and connectors that serves as the vehicle's nervous system.
Understanding the automotive wire harness manufacturing process is essential for OEM project managers and engineers. This process ensures that power and data signals reach every component, from the headlights to the Advanced Driver Assistance Systems (ADAS). Because a single failure can lead to a vehicle recall or safety hazard, the manufacturing workflow is governed by extreme precision and rigorous international standards.

Before a single wire is cut, the manufacturing process begins in the digital domain. Engineering teams use specialized software like CATIA or AutoCAD Electrical to create the vehicle's electrical architecture.
This design phase is where Design for Manufacturing (DFM) principles are applied. By optimizing the layout early, manufacturers can reduce material waste and simplify the eventual manual assembly steps.
Once the design is finalized, the physical production begins with automated wire processing. This stage requires high-speed machinery to ensure repeatability and tight tolerances.
Automated machines pull wire from large reels, measuring and cutting it to precise lengths defined in the 2D drawing. Simultaneously, the machine strips the insulation from the ends. Precision is vital here; if the stripping blade nicks the copper strands, the wire’s conductivity and mechanical strength are compromised.
Crimping is the most critical mechanical step in the automotive wire harness manufacturing process. It involves attaching a metal terminal to the stripped end of the wire.
In automotive environments, terminals must withstand constant vibration and thermal cycling. Manufacturers utilize "Crimp Cross-Sectional Analysis" to ensure the terminal is compressed enough to create a gas-tight seal without over-compressing and weakening the metal.
Large harnesses are often broken down into smaller sub-assemblies to improve efficiency. These sub-units are easier to manage before they are integrated into the main trunk.
Despite advancements in automation, the final assembly of an automotive wire harness remains largely a manual process. This is due to the inherent flexibility of wires and the complexity of the branching paths.
Workers place the processed wires onto a massive "nail board" or "form board." The board features pegs and guides that follow the 2D design layout.
| Feature | Manual Assembly | Automated Processing |
|---|---|---|
| Primary Use | Routing, Taping, Plugging | Cutting, Stripping, Crimping |
| Advantage | Flexibility for complex layouts | High speed and extreme precision |
| Quality Check | Visual and tactile feedback | Sensor-based monitoring |
In the automotive industry, a "zero-defect" policy is the standard. Every harness must undergo a series of tests before it is cleared for shipping to the vehicle assembly plant.
The finished harness is plugged into a test bench configured with the specific mating connectors. A computer runs a low-voltage test to ensure every circuit is complete and that no "cross-talk" or short circuits exist between pins.
Mechanical integrity is verified through pull-force testing on a sampling of crimped terminals. Additionally, highly trained inspectors check the harness against the "Golden Sample" to ensure every clip and label is in the correct orientation.
High-quality manufacturing must adhere to IATF 16949 (Automotive Quality Management) and IPC/WHMA-A-620, which defines the "Requirements and Acceptance for Cable and Wire Harness Assemblies." These certifications act as a guarantee of reliability for Tier 1 and Tier 2 suppliers.
Selecting a manufacturing partner involves evaluating their ability to handle the specific rigors of the automotive environment. Materials must be chosen based on their resistance to oils, extreme temperatures, and mechanical stress.
For instance, specialized automotive wire harness solutions often require customized insulation materials like cross-linked polyethylene (XLPE) for high-heat areas. The manufacturing process must be agile enough to accommodate these material variations while maintaining high throughput.
Furthermore, as the industry shifts toward Electric Vehicles (EVs), the manufacturing process is evolving to include high-voltage orange cabling. These require specialized shielding and orange-coded connectors to ensure technician safety and prevent electrical noise interference with low-voltage logic circuits.


