

2026-10-22
Evaluating an automotive wiring harness supplier means checking whether its engineering, production and quality records support your specific harness. A competitive quotation and a good-looking sample are useful starting points, but approval should also consider process control, traceability and repeatable delivery.
For an existing shortlist, use one representative harness to review each supplier against the same drawing, component requirements and acceptance criteria.
Identify whether the project involves engine wiring, body electronics, diagnostic connections or another subsystem. SOAR’s automotive wire harness collection and electronic wire harness collection provide product-family references.
For a specific example, its SAE J1939 9-pin Y cable assembly gives buyers a configuration to discuss. Confirm the exact pinout, connector variant and vehicle interface before assessing suitability.
If certification is required, verify validity, scope and the site that will manufacture your order. Also identify outsourced processes. A certificate or equipment list alone cannot establish capability for your particular build.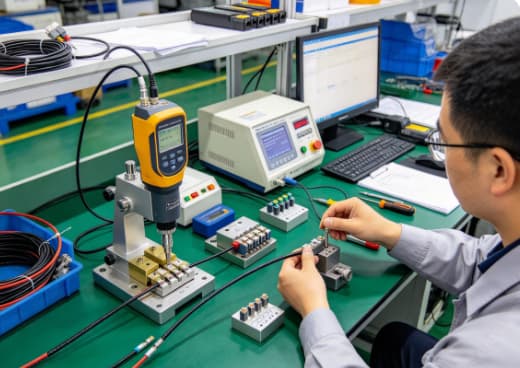
Request records from a comparable project or an agreed trial build. Confidential customer details can be removed while retaining enough information to judge the process.
| Review area | Evidence to request | Warning sign |
|---|---|---|
| Drawing control | Drawing, BOM, pinout and work instructions with matching revisions | Quotation and production documents use different revisions |
| Component control | Approved terminal, connector, wire and seal references | Substitutions require no customer approval |
| Crimping | Applicable specifications, tooling identification and inspection records | Only finished-harness photographs are available |
| Electrical inspection | Test coverage, limits, fixture identification and results | A “pass” result has no defined acceptance criteria |
| Traceability | Links between material lots, production batches and inspection records | Labels cannot be traced to build records |
| Delivery readiness | Material availability, trial-run output and bottleneck review | Capacity claims rely only on machine counts |
For crimped connections, ask how the supplier matches terminals, wire sizes and tooling, sets process parameters and reacts to an out-of-limit result. TE Connectivity’s crimp-height guidance explains why tooling design and maintenance matter to consistent crimp performance.
Request the applicable crimp-height records, visual criteria and pull-test results where specified. Destructive testing should use designated samples under an agreed plan, rather than being described as a test performed on every shipped termination.
For electrical inspection, confirm which circuits are checked for continuity, shorts and pin assignment. Separate routine production checks from qualification tests such as vibration, thermal cycling or sealing validation. Ask what happens to failed parts and how reworked assemblies are retested.
The NASA-STD-8739.4 workmanship standard offers background for critical cable and harness work. Automotive acceptance should follow the applicable customer specifications and agreed workmanship criteria; NASA requirements are not automatically applicable. 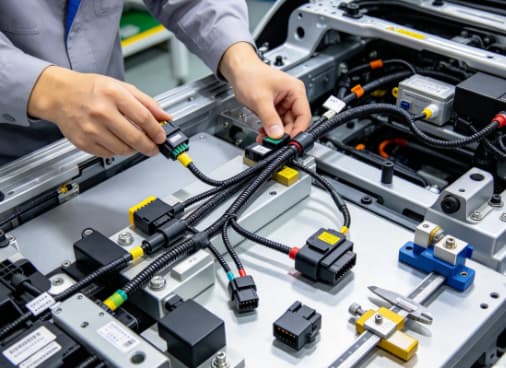
Check connector engagement, branch lengths, mounting positions, protection and label readability on the intended installation or a representative fixture. Record deviations against the drawing rather than approving a sample by appearance alone.
Ask whether the sample uses the intended production materials, tooling and process. If it is a hand-built prototype, identify what must be revalidated during the pilot run.
Where the customer requires it, agree on Production Part Approval Process (PPAP) deliverables before the approval build. AIAG describes PPAP as a way to demonstrate that engineering requirements can be consistently met during an actual production run. Confirm the required submission level and customer-specific evidence.
Ask the automotive wiring harness supplier to trace a finished sample back to its component lots and inspection results. The UL Solutions Wiring Harness Traceability Program provides a reference for cable tracking through the supply chain; participation must be verified separately if required.
Agree which material, tooling, process or manufacturing-site changes need notification and approval. Request a redacted corrective-action example showing containment, root cause and verification that the problem did not recur.
Compare quotations on the same scope: approved components, tooling, testing, documentation and packaging. Confirm connector procurement time, production capacity and forecast assumptions. Record approval as accepted, conditional with dated actions, or pending further evidence; unresolved critical requirements should remain release blockers.
No. Check the relevant site and scope, then review project-specific engineering, production and inspection evidence.
No. Define routine checks, sampled destructive tests and design-validation tests separately, following customer requirements.
Request its exact part number and supporting comparison. Approve the change only after the mating interface, electrical ratings, materials and validation needs are reviewed.
Send your drawing, BOM, pinout, target quantities and supplier-review checklist to request a project review from SOAR. Ask the response to identify proposed components, available inspection evidence and any open requirements before sample approval.


